
Satisfies 1 requirement
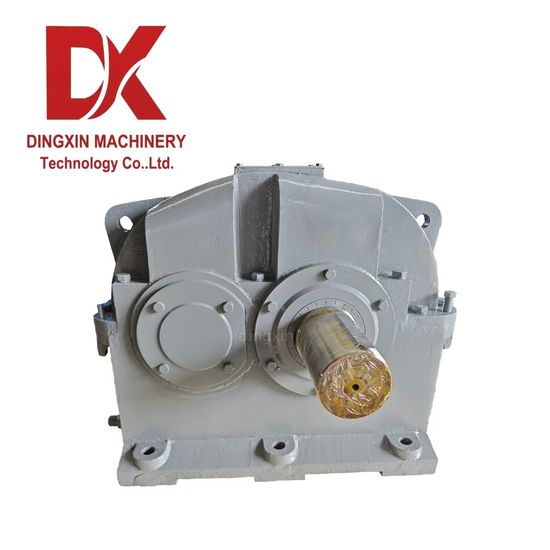
Large Module Customized Carburizing & Quenching Spur Gear Shaft for Metallurgy Equipment
US$100.00-2,999.00
1 Piece(MOQ)
I have found results from100000+products and40000+suppliers aboutCarburizing




When sourcing carburizing solutions, you must prioritize Case Depth (Effective Case Depth), which typically ranges from 0.1mm to 2.5mm depending on the application. Ensure the supplier can guarantee Surface Hardness (usually 58-62 HRC for gear steels) and a Carbon Gradient that prevents brittleness. For equipment, verify the Atmosphere Control System (e.g., oxygen probes or infrared analyzers) to ensure precise Carbon Potential management.
Carburizing is most effective on Low-Carbon Steels and Low-Carbon Alloy Steels with a carbon content typically between 0.10% and 0.25%. Common international grades include AISI 1018, 8620, 4320, and European standards like 16MnCr5 or 20MnCr5. Using the wrong grade can lead to core softening or excessive distortion during the Quenching phase.
Suppliers should strictly adhere to ISO 9001 for general quality management. For automotive components, IATF 16949 is mandatory. Specific process standards such as AMS 2759/7 (for gas carburizing) or CQI-9 (Heat Treat System Assessment) are critical benchmarks for ensuring process repeatability and safety in high-stress applications like aerospace or automotive transmissions.
Compare Gas Carburizing versus Vacuum (Low-Pressure) Carburizing. While Gas Carburizing offers lower initial processing costs and is suitable for high-volume simple parts, Vacuum Carburizing reduces Intergranular Oxidation (IGO) and minimizes Distortion, which can significantly lower Post-Treatment Machining Costs. Calculate the Total Cost of Ownership (TCO) by including the cost of final grinding and scrap rates.
Request a Microstructure Analysis Report and Hardness Profile Chart for every batch. Professional suppliers on Made-in-China.com should provide Third-Party Inspection Reports (e.g., SGS or TUV) that verify the effective case depth via Micro-Vickers testing. Always insist on a Pre-Shipment Sample from the actual production run.
Focus on Energy Consumption Ratios and Maintenance Cycles rather than just the purchase price. Negotiate for a Spare Parts Package (including heating elements and thermocouples) and Remote Technical Support. For large-scale furnaces, request FOB (Free On Board) terms to maintain control over specialized heavy-lift shipping logistics.
Utilize Secured Payment Services provided by reputable platforms like Made-in-China.com to ensure funds are only released upon confirmation of shipping documents. For custom-built furnaces, implement a Milestone Payment Schedule: 30% deposit, 40% after successful factory acceptance testing (FAT), and 30% upon delivery and final inspection.
Carburized parts are highly susceptible to Oxidation and Rust during long-term sea transit. Ensure the supplier uses VCI (Volatile Corrosion Inhibitor) bags or applies a Heavy-Duty Anti-Rust Oil coating. Parts should be packed in Vacuum-Sealed Plastic and secured in Fumigated Wooden Crates to prevent physical impact damage to the hardened surfaces.